Introduction
A masterbatch can look uniform in the pellet bag and still produce streaks, specks or a shade difference when it is used in the final product. The pellet is only one checkpoint. The more important question is whether the concentrate gives the expected result when it is diluted into the production resin.
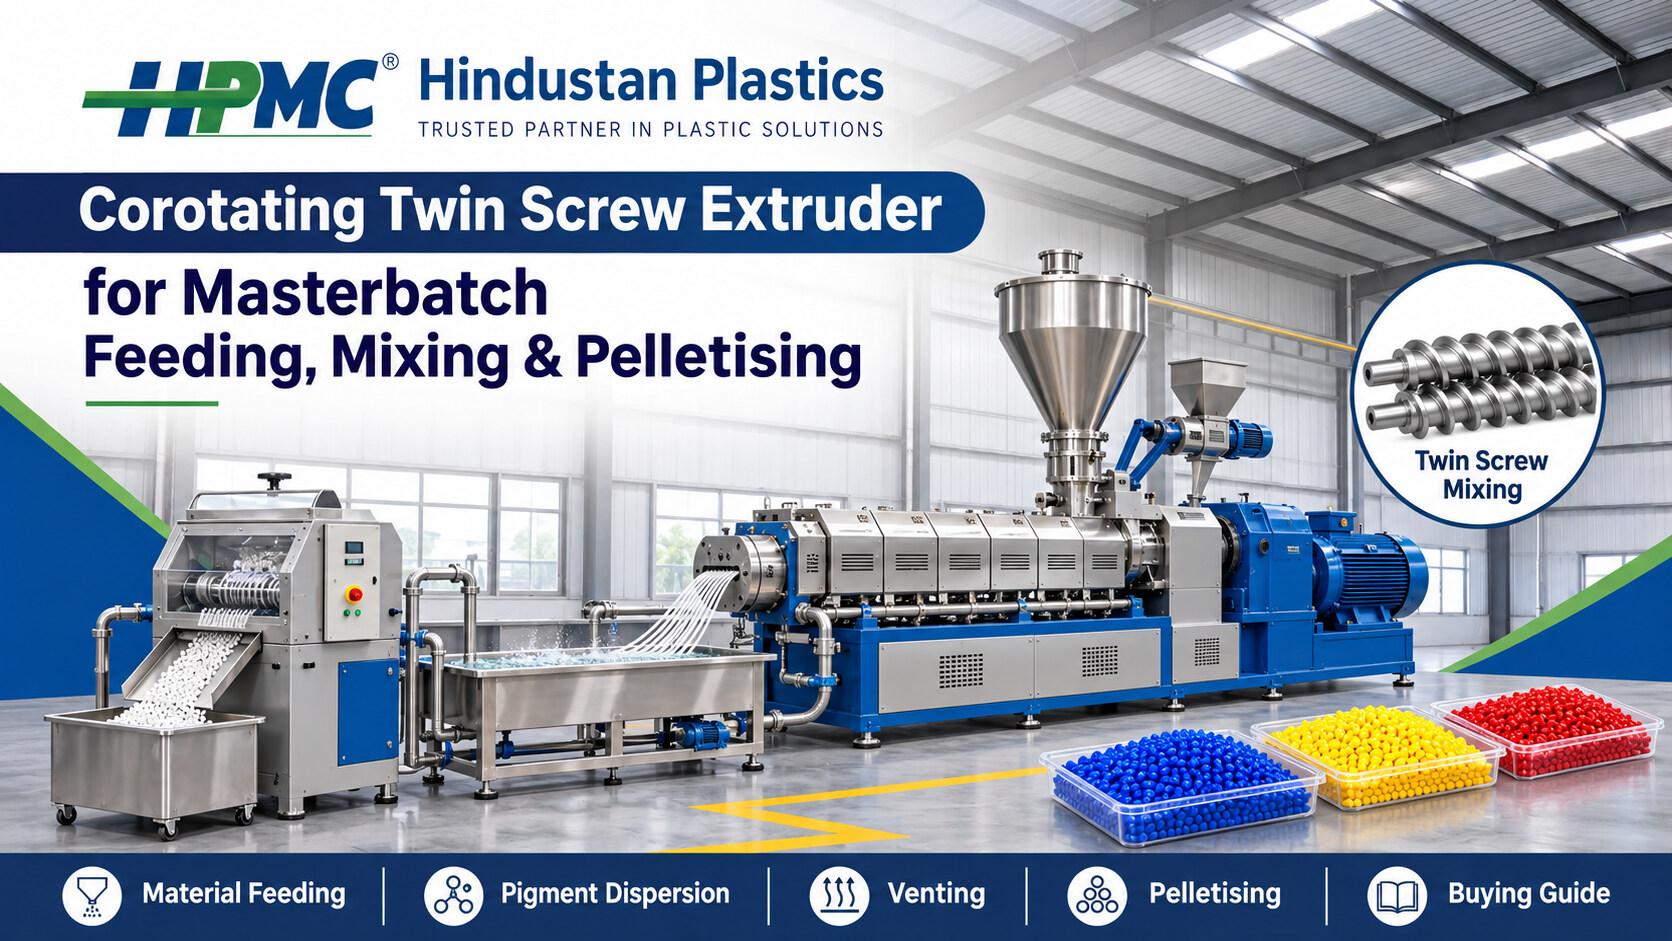
A corotating twin screw extruder for masterbatch production combines a carrier polymer with pigments, fillers or functional additives. The extruder is part of a complete line that also meters the ingredients, handles the melt and turns it into pellets. A change at any of those stages can affect the consistency of the finished concentrate.
This guide explains how the line works, how colour and filler formulations change equipment requirements and what to measure before accepting a supplier’s trial.
What Is a Corotating Twin Screw Extruder for Masterbatch?
Masterbatch is a concentrated mixture of a carrier polymer and one or more pigments, fillers or additives. The customer adds a specified amount of that concentrate to another resin during production. This dilution step is often called let-down. The resulting colour or function depends on the concentrate, the resin it is added to and the conditions used to process them together.
A co-rotating twin screw extruder uses two screws turning in the same direction to convey and mix the formulation. Screw elements can be arranged for different processing tasks, such as conveying material, melting the carrier and mixing the ingredients. The arrangement needs to suit the actual formulation and the output required.
HPMC offers equipment for colour and filler masterbatch applications through its Co-Rotating Twin Screw Extruder. Discuss the complete configuration with the supplier when you share your recipes, intended throughput and quality requirements.
How Does a Masterbatch Extrusion Line Work?
1. Prepare and Meter the Ingredients
Identify the carrier resin, pigment or filler, and any other additives in the recipe. Tell the supplier whether each ingredient is supplied as pellets, powder or another form. Two ingredients that have the same weight in the recipe may feed differently if one flows freely and the other tends to bridge or cling to the feeder.
Ask how the line will meter each ingredient. During a trial, record the intended rate and the actual consumption over a defined period. Check what happens when a hopper is refilled or the rate is changed. If the recipe needs a small amount of a concentrated pigment, ask the supplier to demonstrate feeding at that rate.
2. Choose Between Premix and Split Feeding
In a premix arrangement, selected ingredients are blended before they enter the extruder. The supplier should explain how the blend will be prepared and transferred without introducing unwanted variation. Ask how the blend is handled between the mixer and feeder, especially if the ingredients differ in particle size or bulk density.
In a split-feed arrangement, ingredients enter at different points. For example, a carrier polymer may enter upstream, with a pigment or additive introduced through a side feeder at a later stage. Ask which materials will enter at each point, why the supplier chose that sequence and how the individual feed rates will be checked. Evaluate both routes against the formulation you actually plan to run.
3. Melt the Carrier and Mix the Formulation
The carrier must reach a condition that allows the ingredients to be incorporated and mixed. Screw design, feed rate and temperature settings influence what happens inside the barrel. Ask the supplier to explain the purpose of the proposed mixing sections and to show what adjustments are available when you move between formulations.
For colour concentrates, evaluate whether the pigment is distributed evenly and whether visible specks remain after dilution. For filler concentrates, discuss how the line will incorporate the intended filler loading and how the result will be inspected. HPMC’s Co-Rotating Twin Screw Extruder for Compounding and Recycling describes its broader compounding applications.
4. Check Whether the Recipe Needs Venting
Venting can help remove entrained air or volatiles where the formulation and process call for it. Ask the supplier which part of the recipe creates the need for venting and what preparation is required upstream. If the feedstock needs drying, include that requirement in the trial plan.
Record how the line behaves around the vent during stable production and after a rate change. If material escapes through the vent or bubbles appear in the strand, note the recipe and operating conditions. Give those observations to the supplier so the team can check the cause before changing the setup.
5. Cool and Pelletise the Extruded Material
In strand pelletising, the material exits the die as strands, cools and is cut into pellets. The cooling arrangement and cutter must suit the formulation and line rate. During the trial, observe whether strands break repeatedly and collect samples to check pellet length, fines and visible variation.
Ask what happens after a strand break. Time spent restoring stable operation affects the amount of finished product you can pack during a shift. For details on cooling and cutting, see HPMC’s strand pelletising guide.
What Changes Between Colour, Filler and Additive Masterbatch?
Start with the formulations that will make up most of your production. The equipment priorities can differ even when the finished materials are all sold in pellet form.
- Colour masterbatch. Check pigment feeding, dispersion and shade consistency after dilution. If you run light and dark colours on the same equipment, include cleaning time and the amount of material used to clear the previous colour.
- Filler masterbatch. Check how the filler is fed, how consistently it enters the melt and whether the line can sustain the intended loading and output. Discuss wear parts and maintenance with the supplier using the actual filler and target recipe.
- Additive masterbatch. Identify the active ingredient, its feed rate and any processing limits given by the material supplier. Agree on a test that measures the intended function in the final application.
When you share a product range, distinguish the formulations you will run weekly from grades you plan to make occasionally. Ask the supplier to show how the machine handles the highest-volume recipe and the recipe that places the greatest demand on feeding, mixing or cleaning.
How to Evaluate Masterbatch Quality During a Trial
Agree on the sample preparation and acceptance criteria before the supplier runs the machine. Keep an approved reference where available. A visual comparison of pellets can help identify changes, while testing at the agreed let-down ratio shows how the concentrate behaves in the intended resin.
- Shade consistency. Prepare samples at the same dilution ratio and under comparable processing conditions. Check them against an approved sample or the customer’s agreed colour criteria.
- Dispersion. Inspect the diluted material using the test appropriate to your application. Record where specks or streaks appear and whether they recur across samples.
- Pellet condition. Check pellet size, visible fines and any damaged or irregular pellets. Record differences between material collected before and after an interruption.
- Batch consistency. Take labelled samples from the start, middle and end of the agreed run. Use the same inspection method so differences can be traced to a point in the process.
- Saleable output. Weigh the pellets that pass the agreed inspection. Keep startup material, purge waste and rejects separate so the trial report shows how much usable product was made.
If your customers process the material in film, moulding or another downstream operation, agree on a representative test for that application. Keep the carrier resin, let-down ratio and test conditions the same when comparing batches or suppliers.
Common Masterbatch Problems and What to Inspect
Write down what changed before the problem appeared. A new pigment batch, feeder refill, recipe change or interruption in strand cutting can help narrow down the investigation. Use the following points as a starting guide.
- Shade drift during a run. Compare feed rates, ingredient batches and the preparation of the diluted test samples.
- Specks in the diluted product. Review the pigment or filler condition, mixing setup and possible carryover from the previous recipe.
- Inconsistent feeding. Check how the material moves through the hopper and feeder, including what happens during refilling.
- Repeated strand breaks. Review changes in melt delivery, strand cooling and the path into the cutter.
- Excess fines in the pellets. Inspect the cutter condition, pellet handling and when the fines appeared during the run.
Keep samples from before and after an adjustment. Compare them under the same test conditions and discuss the results with the supplier. This helps separate a change in the extrusion process from a change in how the test sample was prepared.
How to Choose a Corotating Twin Screw Extruder for Masterbatch
1. Define the Recipes You Need to Run
Give the supplier a list of intended carrier resins, ingredient forms and loading ranges. Identify the formulations that need special attention, such as a low-dose pigment or a grade that takes longer to clean out. Ask the supplier to base the equipment proposal on those requirements.
2. Compare the Complete Line Scope
Request an itemised quote for material preparation, feeders, extruder, die, cooling, pelletising and controls. Confirm which equipment is included and what must be purchased separately. If you plan to reuse a feeder or cutter, share its capacity and layout so the supplier can check compatibility with the proposed line.
Ask how the line records feeder rates and production data. A trial record is more useful when it shows which settings were used, how long the run lasted and what material was collected. Agree on which information the operator should record at startup, during stable operation and after a changeover.
3. Measure the Result Over a Defined Run
Compare quotes using the same recipe, time window and acceptance criteria. For example, suppose a one-hour trial produces 160 kg of pellets. If 12 kg comes from startup and 8 kg fails quality checks, the saleable output is 140 kg for that hour. Ask the supplier to report both totals so you can compare the trial with your production plan.
Record downtime as well as material loss. If a supplier reports only the stable period, request the elapsed time from the agreed trial start to its end. A short steady run can show what the line can achieve under those conditions, while the full run shows how interruptions affect usable output.
4. Check Changeover and Cleaning Time
If your plant runs frequent colour changes, include a changeover in the trial. Time the switch from the last approved pellets of one recipe to the first approved pellets of the next. Weigh the material used during the transition and check the diluted sample for carryover.
Ask which areas need cleaning and which parts must be accessed. Discuss the expected procedure with the equipment supplier and confirm what operator training covers. HPMC describes its commissioning and troubleshooting support under Technical Assistance.
5. Plan for Wear Parts and Service
Ask for a list of wear parts for the quoted configuration, including the relevant feeder, screw, barrel or cutter components. Confirm which parts need regular inspection and what identification is needed to order replacements. For service planning, review HPMC’s Spare Parts offering.
How to Plan Production Around Colour Changeovers
List your regular orders by carrier resin, colour and required quantity. Then identify which recipes can run in sequence and which need a full cleanout under the supplier’s procedure. This gives you a schedule you can use when asking for a trial. A machine that performs well on one long run may need a different operating plan when it switches between several short orders.
For example, a factory might produce a dark concentrate and then move to a light shade on the same line. During the changeover, collect and label samples until the light concentrate meets the agreed colour criteria after dilution. Record the time and material used to reach that point. If the next order uses a different carrier, include the additional steps recommended for that material combination.
Use these records to estimate what will be available for packing by the end of a shift. If changeovers take a large share of your available time, compare the proposals against your actual order sequence. Ask each supplier to explain how its proposed feeding and cleaning arrangements support that schedule. Record purge waste for each transition.
What Affects the Price of a Masterbatch Extrusion Line?
The price depends on the line capacity, feeder count, screw and barrel configuration, cooling arrangement, pelletiser and controls. The scope of installation and trials also affects what the quote covers. Ask suppliers to price the same equipment and acceptance requirements so you can see where their proposals differ.
Before comparing proposals, check the details most likely to affect the installation.
- Feeding equipment. Confirm which ingredients need separate feeders and whether those feeders are included.
- Downstream equipment. Check the scope of strand cooling, pellet cutting and pellet collection.
- Utilities and layout. Request the footprint, electrical requirements, cooling needs and access space for routine service.
- Trial and commissioning. Agree on the recipe, trial duration, sample checks and operator training.
Share these requirements in writing. If an item is missing, ask whether it is optional, included elsewhere or something your factory must arrange separately.
Conclusion
Choose a corotating twin screw extruder for masterbatch by starting with your recipes and the quality expected after dilution. Verify how the ingredients feed, how the pellets perform in the final resin and how much saleable output the complete line produces. Include a representative changeover if your plant will switch grades frequently.
Contact HPMC
HPMC (Hindustan Plastics and Machinery Corporation).
Share your carrier resin, pigment or filler details, intended loading, target output and test requirements with HPMC to discuss a suitable masterbatch line configuration.
Address: 5, Category II, DSIDC Industrial Area, Nangloi, Delhi – 110041, India.
Phone: +91 95605 96392.
Email: info@hindustanplastics.com.
Frequently Asked Questions
Find quick answers to the most common questions about this topic.
It processes and mixes a carrier polymer with pigments, fillers or functional additives. The resulting concentrate can be pelletised for use at an agreed dilution ratio.
Premix involves blending selected ingredients before feeding. Split feeding introduces ingredients separately, potentially at different points along the extruder.
Some configurations can support both applications. Confirm the intended recipes, feeder options, screw setup and changeover requirements with the supplier.
A side feeder introduces a selected ingredient at a downstream point in the barrel. Its suitability depends on the recipe and the proposed screw configuration.
Dilute the masterbatch into the agreed resin at the specified ratio and prepare a representative test sample. Inspect it using the method agreed for the intended application.
Venting requirements depend on the material and processing conditions. Ask the supplier what the vent is intended to remove and how the ingredients should be prepared.
Changes in melt delivery, cooling or the strand path into the cutter can contribute. Record when the breaks occur and review the conditions with the supplier.
Weigh the pellets that pass inspection over a defined period. Record startup material, purge waste, rejects and interruptions separately.
The price depends on the extruder configuration, feeders, controls, pelletising equipment and commissioning scope. Request an itemised quote based on your actual formulations.
10. What should I share with HPMC before requesting a quote?